PLC lab · Level 16 of 19
Palletiser sequence
Level 16 of 19 in the PLC lab: a free PLC exercise at Intermediate level, which takes about 1 hour 10 minutes. Count cartons into layers, push each layer onto the pallet, lower the pallet one step, and stop with a lamp when the pallet is full.
Free · no download · about 1 hour 10 minutes. Your work is saved on this device. Updated 18 Oct 2026.
The brief
- Client
- Tamworth Foods
- Site
- Palletiser PAL-1, line 2
- Work order
- TF-2616
- Industry
- Food and drink
- Task code
- PLC-16
- Difficulty
- Intermediate
- Type of work
- Programming
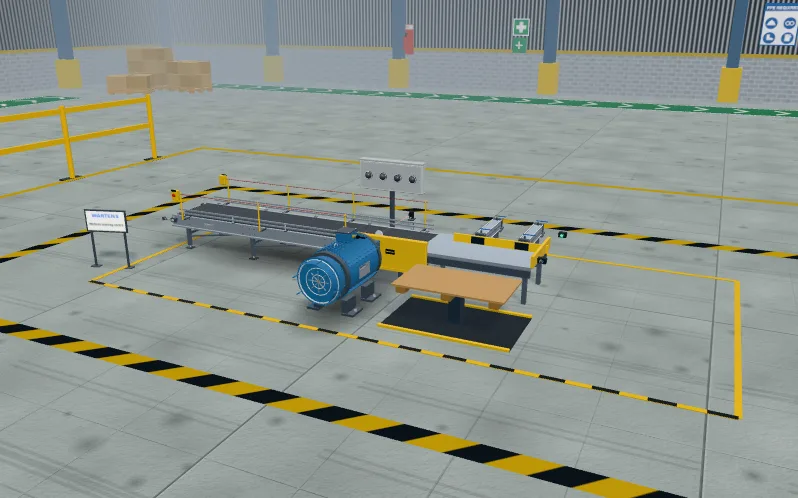
Count cartons into layers with a photo-eye, push each layer onto the pallet, lower the pallet one layer height, and stop with a full-pallet lamp after the last layer. Pushing and lowering must never overlap.
What you do
- Read the client brief and the tag table: 13 tags, 7 inputs and 4 outputs.
- Write the logic in ladder, Structured Text or SFC.
- Press Simulate and watch the plant answer your program.
- Run the factory acceptance test and fix what fails.
Skills you practise
- Step sequencing
- Counting with a one-shot
- Timed output (pallet lowering)
- Interlocking movements
- Limit-switch feedback
What the test checks
The factory acceptance test runs 6 numbered tests against your program. The numbers in the brief are drawn per learner. The tests are:
- Start, Stop and E-stop run the Infeed
- Counts 5 cartons once each and stops the Infeed
- Pushes the layer out and waits for the pusher to come home
- Lowers the pallet for 1800 ms, then starts the next layer
- A full pallet of 2 layers, then Pallet removed
- Stop and E-stop end the cycle, and Start begins a fresh layer
In this lab
- Ladder, Structured Text and SFC in one studio
- A plant that answers: motors, tanks, conveyors
- Numbered tests mark your program
Levels in the PLC lab
Previous: Air handling unit temperature controlNext: Batch mixer with recipes
- Motor start/stop with overload
- Forward/reverse conveyor
- Star-delta fan starter
- Batch counter on a packing line
- Tank filling pump
- Pedestrian crossing
- Parcel sorter
- Duty and standby pumps
- Scale the tank level
- Conveyor jam detection
- Reusable motor block: four motors
- Filling sequence
- Packaging line drive
- Safety gate interlock
- Air handling unit temperature control
- Palletiser sequence
- Batch mixer with recipes
- Bottling line: fill, cap, reject
- Fault-finding challenge
Part of the PLC lab
Program a working machine in ladder, Structured Text or SFC and watch it run.
Feeds these internships: PLC Programming.